
Last updated: August 10, 2026
Key Takeaways for Complex HDI DFM
- DFM for 8–20+ layer HDI boards requires early integration of stack-up symmetry, microvia hierarchy, copper balance, impedance control and thermal planning to avoid costly late-stage redesigns.
- Partnering with the fabricator at the stack-up stage prevents warpage, impedance drift and solder-joint stress caused by asymmetry or unbalanced copper distribution.
- Microvia aspect ratios must stay at or below 1:1, with 0.8:1 as the practical target, and staggered configurations improve thermal reliability in fine-pitch BGA designs.
- Via-in-pad fill-and-cap specifications, back-drilling, solder-mask clearances and test-point access must be finalized during DFM review rather than assumed in layout.
- Pro-Active Engineering embeds manufacturing engineering into the design phase and offers a single accountable workflow for complex, regulated programs. Start a DFM review with the engineering team.
HDI DFM Guidelines for Early Stack-Up Decisions
The first HDI DFM decision is stack-up selection, and it must be made in partnership with the fabricator. A symmetrical stack-up is the single most important rule for avoiding warpage because unbalanced copper and uneven dielectric thickness cause the board to bend during lamination and reflow. Symmetry means the construction above the board centerline mirrors the construction below it, including copper weight, dielectric thickness and material type.
Asymmetry, broken reference planes, unclear material substitutions and copper distribution that ignores lamination behavior are the stack-up mistakes most likely to cause bow, twist, impedance drift and solder-joint stress on high-layer-count boards.
Pro-Active Engineering embeds manufacturing engineering into the design phase, so stack-up decisions reflect actual fabrication constraints from day one. This approach reduces design iterations and supports a predictable path to production.
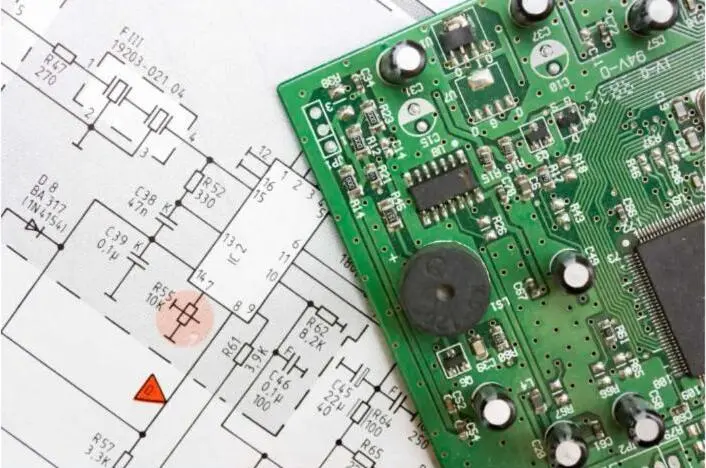
Start a stack-up review with Pro-Active’s engineering team.
Via-in-Pad DFM and Microvia Aspect Ratio Rules
IPC-T-50M defines a microvia as a blind structure with a maximum aspect ratio of 1:1 and a total depth of no more than 0.25 mm. Reliable copper plating inside these structures depends on maintaining a favorable aspect ratio, the relationship between depth and diameter.
IPC-2226 specifies a maximum microvia aspect ratio of 1:1 for reliable copper plating, but manufacturer guidance generally targets 0.8:1 as the practical working limit. Ratios above 0.8:1 produce progressively thinner plating at the bottom corner that cracks under thermal cycling, with 1:1 as the absolute limit rather than a design goal.
Via hierarchy matters as much as individual aspect ratios. Staggered microvias are preferred over stacked configurations for high-reliability applications because staggered structures distribute thermal stress across a wider area and achieve more thermal cycles to failure. Sequential lamination enables multi-level microvia builds. A 1+N+1 structure adds one microvia layer per side, while 2+N+2 supports deeper interconnect hierarchies for boards targeting fine-pitch BGAs.
Pro-Active’s advanced interconnect capabilities include tight-tolerance microvia structures and sequential lamination builds engineered for aerospace, defense and other high-reliability programs.
Copper Balancing for High-Layer and Controlled-Impedance Boards
Copper balance is a fabrication requirement, not a layout preference. If copper weight, dielectric thickness or material type differs significantly above and below the centerline, the board can exhibit increased movement during fabrication and reflow. Copper balance becomes even more critical on controlled-impedance designs, where tight geometric tolerances leave no margin for the board movement that unbalanced copper causes.
Each high-speed signal layer requires a nearby continuous reference plane and a controlled return path to prevent return-current detours during via transitions. Material callouts must include the laminate family, performance class, copper weight, impedance requirements and substitution approval rules. Vague callouts invite unauthorized material swaps that shift impedance outside tolerance.
Pro-Active’s thermal-optimized PCB architecture integrates copper balance, reference-plane continuity and impedance control into a single design review. This integration eliminates gaps that appear when layout and fabrication are handled by separate teams.
BGA Escape Routing DFM for Fine-Pitch Arrays
With stack-up, copper balance and impedance control established, the next DFM challenge is routing high-density component interconnects. Ball pitch directly dictates fanout method. Standard through-hole dog-bone fanout suits pitches at or above 1.0 mm. Mixed blind via and through-hole in a 1+N+1 HDI stack-up handles 0.65 mm pitch. Micro-blind via HDI in 1+N+1 or 2+N+2 addresses 0.5 mm pitch. Any-layer HDI or substrate-level fanout is required at or below 0.4 mm pitch.
Via-in-pad is commonly used when BGA pitch is too fine for conventional fanout, and vias must be filled with epoxy and capped with copper to create a flat, solderable surface. Without proper fill and cap, solder wicks into the barrel and starves the joint, which creates assembly reliability problems.
High-speed channels add another requirement. Back-drilling removes via stubs on these nets to reduce signal reflections and improve signal integrity. Because via-in-pad and back-drilling impose tight geometric constraints, design rules for minimum drill size, pad diameter and keep-out areas must be finalized during the DFM review stage rather than assumed in layout. Back-drill requirements must be explicitly flagged in fabrication notes to ensure proper review.
High-speed SerDes BGA escape routing prioritizes differential pairs and clocks, maintains symmetric trace lengths and spacing, and places one adjacent ground return via per high-speed signal via.
Pro-Active’s Speed Shop delivers production-ready prototypes using the same processes as full-scale builds, so BGA escape routing validated in the prototype phase transfers directly to production without process-change risk.
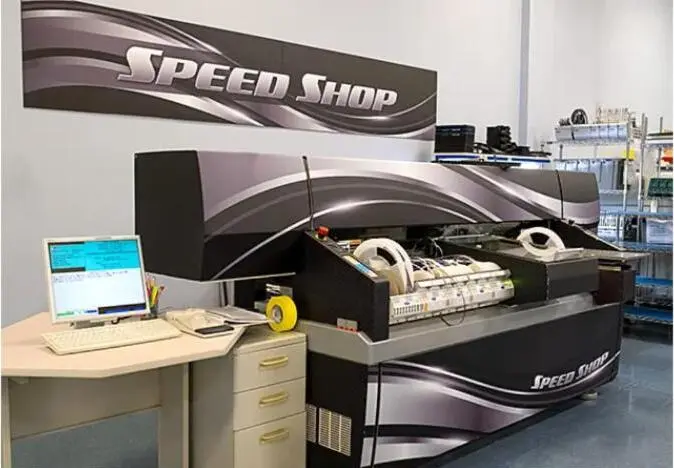
Validate BGA escape routing with a Speed Shop prototype before committing to volume production.
Solder Mask, Silkscreen and Test-Point Strategy for Fine Pitch
Non-solder-mask-defined pads are generally preferred over solder-mask-defined pads for BGA locations because they increase the solderable area and improve joint reliability. Solder-mask apertures must clear the pad without encroaching on adjacent pads, a tolerance that tightens significantly at fine pitch.
Silkscreen placement must not overlap pads or solder-mask openings. On dense boards, silkscreen often reduces to reference designators only, positioned to survive automated optical inspection without creating false-call noise.
DFM review before quoting identifies trace-width violations, pad-to-component clearance issues and test-point access problems to prevent first-article yield losses on complex boards. Test points must be accessible to in-circuit test fixtures and sized to IPC-A-610 Class 2 or Class 3 requirements depending on the program.
Pro-Active holds ISO 9001:2015, AS9100, ITAR, JCP and Nadcap certifications. Every assembly passes 100% automated optical inspection, and flying probe, in-circuit and functional testing are available as part of the integrated workflow.
ITAR and AS9100 DFM Requirements for Regulated Programs
Defense programs require ITAR registration, controlled documentation and U.S.-only manufacturing to meet contracting officer requirements. DFM on regulated programs functions as both a manufacturability exercise and a compliance exercise. Design data, material records, process parameters and inspection results must be traceable from first article through end of life.
Aerospace programs require AS9100-aligned documentation, environmental stress testing and full material traceability, with PCB testing records serving as audit artifacts for the end customer. AS9100 DFM requirements mean that design reviews, nonconformance records and corrective actions form part of the manufacturing data package, not afterthoughts.
Pro-Active operates as a single accountable partner for regulated programs. ITAR-registered manufacturing, controlled documentation, access controls aligned with DDTC requirements and personnel training records are embedded in the production workflow, not bolted on at audit time. SiliconExpert BOM scrubbing and SAE AS5553B counterfeit avoidance methodology protect material integrity across the supply chain.
Final Manufacturing Data Review: DFM Sign-Off Workflow
A complete DFM sign-off package addresses every layer of the design before fabrication release. The following sequence mirrors the review order used by experienced manufacturing engineers on complex HDI programs, starting with foundational stack-up decisions and progressing through interconnect design, signal integrity, assembly requirements and compliance documentation.
- Confirm stack-up symmetry and copper balance across the centerline
- Verify microvia aspect ratios against fabricator capability limits
- Confirm via-in-pad fill and cap specification in fabrication notes
- Flag back-drill requirements on all high-speed channels
- Validate controlled-impedance trace geometry against stack-up
- Check reference-plane continuity at every via transition
- Confirm BGA pad definition and solder-mask apertures
- Verify annular ring compliance for IPC Class 2 or Class 3 as applicable
- Confirm test-point size, location and in-circuit test fixture access
- Review silkscreen clearance from pads and solder-mask openings
- Validate thermal path design and high-power copper integration
- Complete traceability and compliance documentation package
Pro-Active Engineering Capability Ranges
Pro-Active supports multilayer HDI builds, sequential lamination, microvia hierarchy, via-in-pad, back-drilling, fine-pitch BGA escape routing, flip chip, wire bonding, hybrid high-density assemblies, silver sintering, direct thermal path technology, metal-core constructions and heavy copper integration. The company also supports ITAR-registered manufacturing, AS9100 documentation, JCP certification, Nadcap accreditation, full traceability and NIST 800-171 aligned and CMMC readiness controls. These capabilities serve aerospace, defense, industrial, space, medical, power and energy programs.
Downloadable DFM Checklist for Complex Boards
DFM Checklist for Complex PCB Designs
Use this checklist before releasing manufacturing data on any HDI, fine-pitch BGA or controlled-impedance board. This quick-reference list condenses the full sign-off workflow into nine core checks.
- Stack-up symmetry confirmed with fabricator
- Copper balance verified across all layers
- Microvia aspect ratios within fabricator capability
- Via-in-pad specified as filled and capped in fabrication notes
- Back-drill requirements flagged on all critical nets
- Controlled-impedance traces matched to stack-up
- Reference planes continuous at all via transitions
- Test points sized and located for in-circuit test access
- Compliance and traceability documentation complete
Share this checklist with Pro-Active’s engineering team to begin a DFM review.
Conclusion: Reducing Late-Stage Risk with One Domestic Partner
Well-executed DFM redesigns achieve meaningful reductions in total cost, part count and assembly time when manufacturability is addressed at the design stage, not after first-article failures surface.
On 8–20+ layer HDI boards with fine-pitch BGAs, controlled impedance and regulated program requirements, late-stage DFM discoveries create redesign cycles that compress schedules and inflate program cost. Teams that embed thermal optimization and design constraints early converge on robust, manufacturable architectures faster and avoid late-stage layout-driven compromises.
Pro-Active Engineering integrates DFM, advanced interconnect, thermal management and compliance documentation into a single workflow from initial layout through certified production. The Speed Shop delivers production-ready prototypes on short lead times using the same processes as full-scale builds, so what works in development scales without process-change risk. One domestic partner. One accountable workflow. Full traceability from day one.
Connect with Pro-Active Engineering to start a DFM review on a complex PCB program.
Frequently Asked Questions
What is the difference between DFM for standard multilayer boards and DFM for HDI boards?
Standard multilayer DFM focuses on trace clearances, drill sizes and panelization. HDI DFM adds complexity that covers microvia hierarchy, sequential lamination planning, via-in-pad fill specifications, back-drill requirements and stack-up symmetry for warpage control. Fine-pitch BGAs and controlled-impedance requirements further tighten every tolerance. On HDI boards, DFM must be resolved in partnership with the fabricator before layout begins, not reviewed after Gerbers are released.
How does Pro-Active Engineering integrate DFM into the design phase?
Pro-Active’s engineering and manufacturing teams operate within a single workflow. Design engineers, manufacturing engineers and quality personnel collaborate from the first stack-up discussion through final data release. DFM inputs, including fabricator capability limits, material selection, thermal path planning and compliance documentation requirements, are embedded in the design phase rather than applied as a post-layout review. This integration reduces redesign cycles and supports a predictable transition from prototype to production.
What certifications does Pro-Active Engineering hold for regulated PCB programs?
Pro-Active Engineering holds ISO 9001:2015 and AS9100 certifications, ITAR registration, JCP certification (DD Form 2345) and Nadcap accreditation. The company is also aligned with NIST 800-171 and maintains CMMC readiness. Workmanship standards follow IPC-A-610 Class 2 and Class 3, J-STD-001 and IPC-7711/7722. These certifications support defense, aerospace and other regulated programs that require controlled documentation, full traceability and U.S.-only manufacturing.
Can Pro-Active Engineering handle both rapid prototyping and volume production on the same program?
Pro-Active’s Speed Shop delivers production-ready prototypes using the same equipment, materials and processes as full-scale production builds. The prototype phase validates the actual production process rather than a simplified approximation. When a program scales from prototype to volume, there is no process-change risk and no requalification cycle. Pro-Active manages low-to-high volume production with the same quality management system and traceability infrastructure used in prototyping.
What thermal management capabilities does Pro-Active Engineering offer for high-power PCB designs?
Pro-Active provides engineered thermal solutions including silver sintering, direct thermal path PCB technology, advanced metal-core constructions, heavy copper integration and integrated dielectric structures. These capabilities address high-current and thermally demanding applications where standard FR-4 constructions are insufficient. Thermal path planning is integrated into the DFM process, so heat dissipation strategies are resolved at the design stage rather than addressed after field failures or thermal test failures surface.