

Last updated: August 19, 2026
Key Takeaways for Engineering Teams
- InstantDFM performs file-level design rule checks but does not own assembly, traceability or production quality.
- Engineering teams gain better outcomes when a partner embeds DFM review into the active design phase instead of after layout lock.
- Pro-Active Engineering builds prototypes on the same SMT lines and inspection protocols used for full production, which closes the gap between development and scale.
- ITAR registration, AS9100 certification and full traceability documentation under one quality system support defense, aerospace and medical-device programs.
- Start a DFM review with Pro-Active Engineering to experience the advantages of an integrated manufacturing partner.
Six Criteria for Selecting an InstantDFM Replacement
Engineering managers and program leaders evaluating alternatives should apply six criteria to any candidate partner. These criteria separate file-checking tools from integrated manufacturing partners by measuring whether a vendor can support the full program lifecycle from design review through compliant production instead of validating files at a single checkpoint.
- DFM integration: The partner embeds manufacturability review into the design phase instead of checking files after the design is locked.
- Prototype fidelity: Prototypes run through full production processes so successful development builds scale without redesign.
- Compliance posture: The partner holds ITAR registration, AS9100 certification and the traceability infrastructure regulated programs require.
- Engineering depth: The partner handles advanced interconnect, thermal management and high-density assemblies without heavy subcontracting.
- Supply-chain control: One quality system governs sourcing, counterfeit avoidance and component lifecycle risk.
- Lifecycle accountability: A single partner owns the program from design through production instead of handing off responsibility between vendors.
The sections below explain how Pro-Active Engineering addresses each criterion.
Integrated DFM and Prototyping Instead of File Checking
Pro-Active Engineering integrates DFM into the design phase rather than treating it as a file check after layout is complete.
Pro-Active engineers review pad geometry, component orientation, panelization, thermal relief, test-point access and sourcing risk while the design remains open. This timing matters because catching issues inside a single workflow before a file leaves the building separates integrated DFM from a standalone checker that flags problems only after layout lock.

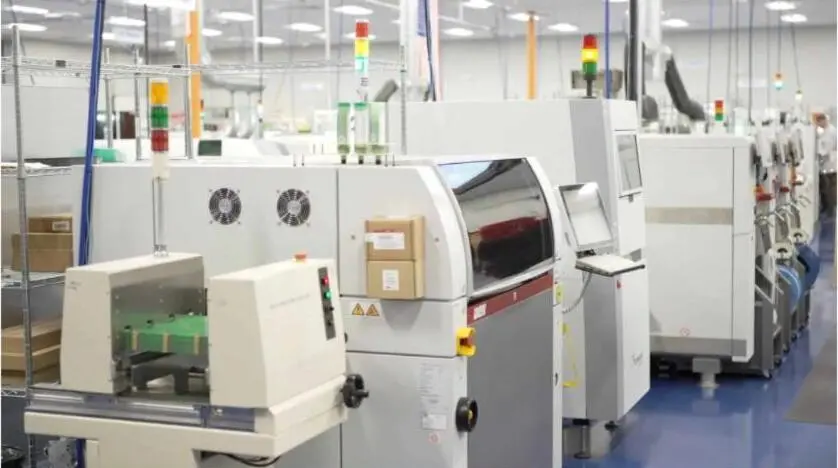
Prototypes built through Pro-Active’s Speed Shop use the same SMT lines, reflow profiles, inspection protocols and documentation controls as full production runs. This approach prevents a common failure mode in which boards that work on an engineer’s test bench fail on the assembly line when prototypes are hand-soldered or built outside production conditions. Speed Shop builds prevent that gap by treating every prototype as a production event from the start.
Start a DFM review on a current design with Pro-Active Engineering.
Domestic ITAR-Compliant Workflow for Regulated Programs
ITAR, administered by the U.S. Department of State, requires that PCB assemblies for items on the United States Munitions List be manufactured by an ITAR-registered facility in the United States to control export of defense-related articles, services and technical data. Pro-Active Engineering is ITAR-registered and maintains access controls, data-handling procedures, documentation practices and personnel training records that defense and aerospace programs require.

AS9100D builds on ISO 9001 with aerospace-specific requirements that cover full material and process traceability, configuration control, risk management at every production stage, counterfeit parts prevention and auditable records from sourcing through final test and delivery. Pro-Active holds these certifications along with ISO 9001:2015, JCP certification and Nadcap accreditation, and operates with NIST 800-171 alignment and CMMC readiness.
Traceability runs through every stage of the Pro-Active workflow. AS9100 Rev D Clause 8.5.2 requires identification and traceability appropriate to the product, with aerospace programs commonly expecting material certifications, special process records and production sequence documentation. Pro-Active’s quality system produces that documentation as a standard output, not a special request. BOM scrubbing through SiliconExpert and counterfeit avoidance under SAE AS5553B sit inside the sourcing process rather than as late-stage checks.
For medical-device programs, the FDA’s Quality Management System Regulation took effect on Feb. 2, 2026, incorporating ISO 13485:2016 by reference and aligning U.S. requirements with validated processes, documentation, traceability and risk management. Pro-Active’s quality infrastructure supports those expectations across regulated industries.
Short-Turn Production-Ready Prototypes Through Speed Shop
Pro-Active’s Speed Shop operates as a dedicated fast-turn line with a minimum order quantity of one unit. It runs SMT and through-hole assembly while maintaining the production-process fidelity described earlier, and AOI is included on every build.

Prototype boards built outside production conditions often expose layout issues only after boards run through high-speed pick-and-place machines and reflow ovens. Those issues then require a comprehensive DFM review to identify spacing problems, thermal imbalances or incorrect land patterns that cause defects and high scrap rates at scale. Speed Shop builds surface those issues at the prototype stage, where corrections remain fast and inexpensive.
Domestic PCB fabricators can often deliver prototype boards in days, which supports faster iteration and shorter development cycles compared with offshore fabrication. Pro-Active’s domestic footprint in Sun Prairie, Wisconsin supports that speed without the IP risk, geopolitical exposure or logistics uncertainty of offshore sourcing.
Because Speed Shop builds use production processes, the transition from prototype to low-to-mid volume production becomes a scheduling event rather than a re-engineering event. The process already runs in a validated state. The documentation already exists. Scale occurs without a handoff to a new vendor.
Engineering Depth and Manufacturing Scope for Complex Programs
Pro-Active’s capabilities extend beyond standard PCB assembly and support complex, mission-critical hardware. The company provides wire bonding, flip chip assembly and hybrid high-density assemblies for programs that require compact, high-reliability interconnect performance.

Thermal management solutions include silver sintering, direct thermal path technology, advanced metal-core constructions and heavy copper integration. These approaches support high-current and thermally demanding applications where standard assemblies struggle to meet performance or reliability targets.
Class 3 workmanship standards for safety-critical, high-vibration or continuous-uptime service tighten annular ring, plating, via fill and solder-joint criteria. Pro-Active assembles to IPC-A-610 Class 2 and Class 3 standards, with rework and repair under IPC-7711/7722 and soldering under J-STD-001.
Electronics account for roughly 82% of documented counterfeit events in the supply chain. Pro-Active’s SAE AS5553B counterfeit avoidance methodology and SiliconExpert BOM scrubbing address that risk at the sourcing stage before a suspect component reaches the line.
Supply-Chain Resilience and Lifecycle Support Under One Roof
Vertically integrated EMS providers give OEMs a single point of accountability, reduced vendor management overhead, clearer communication and stronger IP protection compared with fragmented models that split responsibilities across vendors. Pro-Active operates that model across a 45,000-square-foot facility where design, prototyping, assembly, coating, testing and box build share one quality system and one management team.
Global PCB manufacturers face extended base-material lead times, with materials often available only on an allocation basis. Pro-Active’s integrated sourcing function monitors component lifecycle risk, identifies EOL and NRND parts early and maintains approved alternate MPNs to reduce the chance that a single-source disruption halts a program.
A single accountable partner maintains an integrated view of the full bill of materials, which supports coordinated decisions on EOL, obsolete and long lead-time components and reduces operational risk and unexpected build delays. That coordination sits inside Pro-Active’s standard program management process rather than as an add-on service.
How Pro-Active Compares to Other EMS and Design Options
Large EMS providers prioritize high-volume production. Programs below a volume threshold often receive less engineering attention, slower prototype turnaround and limited DFM collaboration. In fragmented EMS setups, product development slows because of handoffs between design firms, prototype vendors and manufacturing partners. Pro-Active’s high-mix, variable-volume model serves low-to-mid volume programs with the same engineering rigor applied to larger runs.
Design-only firms produce layouts and documentation but do not carry production ownership. When a design transfers to a separate assembler, DFM assumptions made during layout may not match what happens on the line. Pro-Active’s engineering and manufacturing teams operate within one workflow, so DFM decisions made during design carry through into production.
Local job shops offer proximity and flexibility but often lack advanced interconnect capabilities, Class 3 workmanship standards, automated inspection infrastructure and compliance certifications that defense, aerospace and medical-device programs require. Partner selection for PCB manufacturing increasingly emphasizes responsiveness, quality control and proximity instead of unit price alone as program teams account for total landed costs such as rework, compliance gaps and delayed launches.
Share project requirements with Pro-Active Engineering for an integrated review.
Addressing Common Concerns About Switching Partners
Program managers often raise lead-time concerns when evaluating a new manufacturing partner. Pro-Active’s Speed Shop delivers production-ready prototypes on short turnaround through dedicated fast-turn SMT and through-hole lines. Production runs schedule through Manex ERP, which provides real-time operational analytics and transparent status reporting throughout a program.
Pricing comparisons with offshore providers or high-volume CMs often focus on unit cost instead of total program cost. Vertical integration improves total cost control over time through lower coordination and logistics expenses, reduced rework and scrap from early issue detection, fewer expediting charges and more transparent cost structures. Eliminating vendor fragmentation, rework cycles and compliance remediation often offsets a per-unit cost difference over the life of a program.
Engineering teams concerned about losing design control gain an extension of the in-house team. Design reviews, real-time updates and transparent documentation are standard. The customer retains full oversight while accessing 30 years of PCB design and manufacturing experience.
Onboarding disruption presents a legitimate concern. Pro-Active’s standard approach starts with a pilot project to demonstrate performance before shifting production. Many programs see rapid improvements in quality, communication and turnaround during the pilot phase. Teams that scale manufacturing more smoothly often begin building supplier relationships and communication loops during the prototype phase instead of treating supply chain as a later-stage task.
Conclusion: Selecting a True InstantDFM Alternative
InstantDFM serves a narrow function as a file-level design rule checker before fabrication. Engineering teams that need a partner to own DFM from design through production, deliver production-ready prototypes on short turnaround and maintain full compliance traceability under ITAR, AS9100 and related standards require a different model.
Pro-Active Engineering meets all six evaluation criteria outlined above. DFM sits inside the design phase. Prototypes use full production processes. The compliance infrastructure described earlier covers ITAR, AS9100, ISO 9001:2015, JCP and Nadcap. Advanced interconnect and thermal management capabilities support high-complexity programs. Sourcing and counterfeit avoidance operate under one quality system. One partner owns the program from concept through production.
For engineering managers, hardware engineers and program leaders at defense, aerospace and medical-device firms, that single-workflow model reduces program risk, shortens development cycles and closes compliance gaps that fragmented vendor chains create.
Submit project details for an initial engineering review with Pro-Active Engineering.
Frequently Asked Questions
What makes Pro-Active Engineering a true alternative to InstantDFM?
InstantDFM checks design files against fabrication rules. Pro-Active Engineering integrates DFM into the active design phase, so engineers review pad geometry, component placement, panelization, thermal management and sourcing risk while the design remains open and changes stay inexpensive. Pro-Active then builds prototypes using full production processes through the Speed Shop, so the transition to low-to-mid volume production does not require re-engineering. One partner owns the program from design through production under the certifications outlined above. That end-to-end accountability distinguishes an integrated partner from a file-checking tool or a standalone assembler.
How does Pro-Active Engineering support ITAR and AS9100 compliance?
Pro-Active is ITAR-registered and maintains access controls, data-handling procedures, documentation practices and personnel training records that defense and aerospace programs require. AS9100 governs quality, traceability, risk management and counterfeit parts prevention across every production stage. BOM scrubbing through SiliconExpert identifies EOL and NRND components early. Counterfeit avoidance follows SAE AS5553B methodology. Traceability documentation appears as a standard workflow output, covering material certifications, process records and production sequence documentation. NIST 800-171 alignment and CMMC readiness support programs that handle Controlled Unclassified Information.
Can Pro-Active Engineering handle advanced interconnect and thermal management requirements?
Pro-Active provides wire bonding, flip chip assembly and hybrid high-density assemblies for programs that require compact, high-reliability interconnect performance. Thermal management capabilities include silver sintering, direct thermal path technology, advanced metal-core constructions and heavy copper integration for high-current and thermally demanding applications. These capabilities operate under the same roof as PCB design, rapid prototyping, standard SMT and through-hole assembly, conformal coating and box build, so programs with advanced requirements do not need a separate specialty vendor.
What happens when a program scales from prototype to higher volume production?
Because Speed Shop prototypes use the same equipment, processes, inspection protocols and documentation controls as full production runs, scaling becomes a scheduling event rather than a re-engineering event. The process already runs in a validated state. The documentation already exists. Pro-Active’s high-mix, variable-volume manufacturing capability supports programs from a single prototype unit through low-to-mid volume production runs, with the same engineering team maintaining continuity across the program lifecycle. Customers avoid transferring to a new vendor or restarting qualification when volume increases.
Can Pro-Active Engineering serve programs outside the Upper Midwest?
Pro-Active serves customers nationwide from its Sun Prairie, Wisconsin facility. The domestic location supports faster delivery to many U.S. regions compared with offshore sources, and logistics processes support complex, multi-location distribution requirements. For defense and aerospace programs, domestic manufacturing also reduces IP risk, geopolitical exposure and long logistics cycles associated with offshore production. Programs that require an ITAR-registered, AS9100-certified domestic partner are not limited by geography.